 Industry News
Aerospace Honeycomb Panels: Why Vacuum Brazing Is the Only Way to Do It Right
Normantherm•10/13/2026
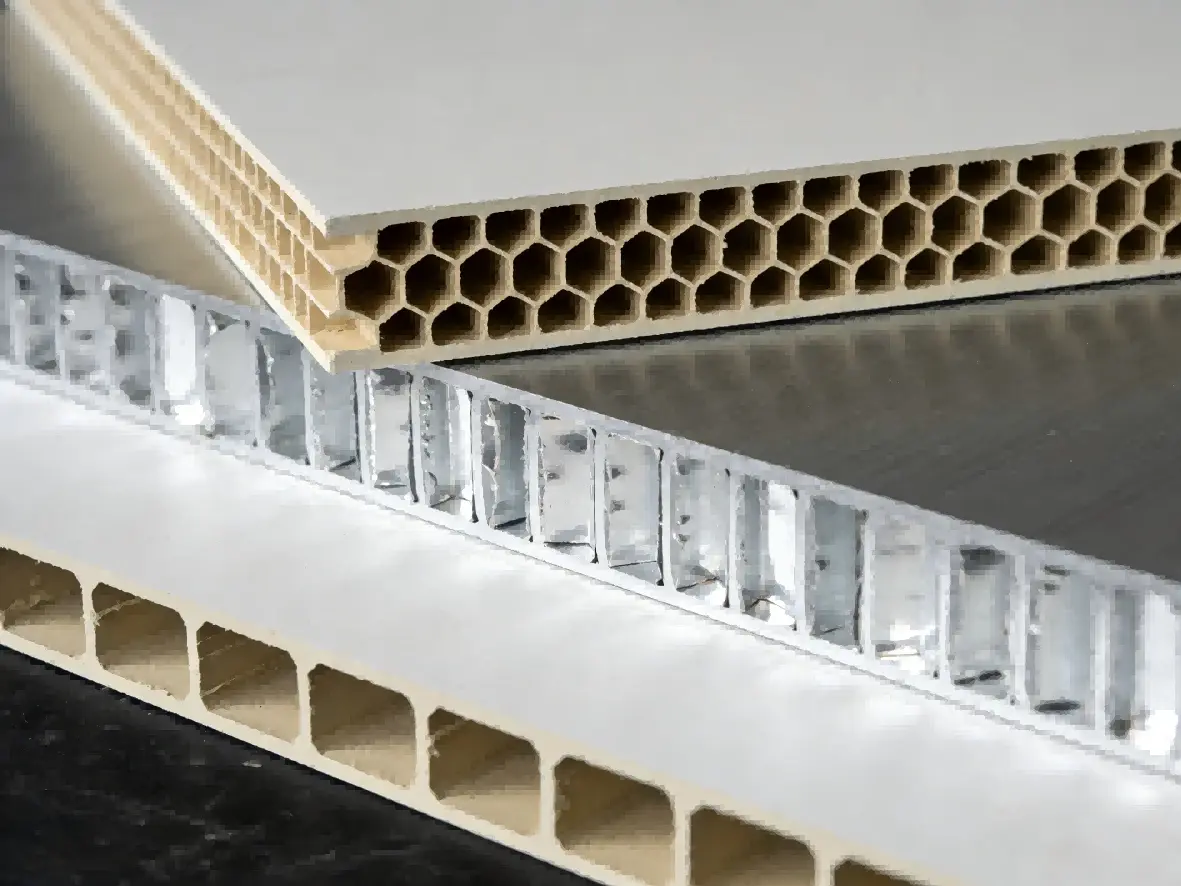
From aircraft floor panels and engine nacelles to spacecraft thermal shields and helicopter rotor blades, vacuum-brazed honeycomb panels are everywhere in modern aerospace manufacturing. If your facility is not using vacuum brazing for these components, you are either outsourcing quality or compromising on it.
What Are Aerospace Honeycomb Panels?
A honeycomb sandwich panel consists of a lightweight hexagonal-cell core, typically aluminum, titanium, or stainless steel, bonded between two thin face sheets. The geometry gives the panel an exceptional strength-to-weight ratio, making it one of the most efficient structural materials ever engineered.
The challenge lies in joining the core to the face sheets across thousands of tiny contact points, simultaneously, uniformly, and without adding weight or compromising integrity. Vacuum brazing is the only process that achieves all of this in a single furnace cycle.
Why Vacuum Brazing?
Many manufacturers begin with adhesive bonding. It is cheap and simple, but it fails at elevated temperatures, degrades under moisture, and cannot meet the structural certifications required for primary aerospace structures. Welding is impractical at the scale and geometry of honeycomb cores.
Vacuum brazing solves every limitation:
Metallurgical bonds at every core-to-face sheet contact point, far stronger than adhesives
No flux, no contamination, no post-braze cleaning required
Handles complex multi-layer assemblies in a single furnace run
Compatible with aluminum, titanium, and nickel superalloy panels
Produces a clean, bright finish, ready for inspection or coating
Where Are These Panels Used?
Aircraft fuselage and floor panel assemblies
Engine nacelles, thrust reversers, and acoustic liners
Helicopter rotor blades and tail sections
Spacecraft thermal protection and satellite structural panels
Missile fins, radomes, and control surface structures
Defense vehicle armor and ballistic panels
The Vacuum Brazing Process for Honeycomb Panels
Getting a honeycomb panel right in the furnace requires absolute control at every stage. Here is how it works in a Normantherm vacuum brazing furnace:
Assembly & fixturing, panels are assembled with brazing alloy foil or clad face sheet and fixtured to maintain contact pressure across the entire surface
Controlled ramp-up, gradual, multi-step heating prevents thermal shock and distortion of the thin core walls
Brazing soak, held at precise temperature (typically 580–620°C for aluminum alloys) long enough for full filler flow
Controlled cooling, slow, uniform cool-down locks in the braze and prevents warping
The entire cycle is automated, logged, and fully repeatable, essential for aerospace quality certification and batch traceability.
Why Manufacturers Choose Normantherm
Normantherm vacuum brazing furnaces are engineered specifically for the demands of aerospace-grade panel production:
Temperature uniformity ±3°C across the full hot zone, verified and certified
Vacuum levels to 10⁻⁵ mbar, ensuring oxide-free, flux-free joints
Large flat hot zones available, accommodating full-size aerospace panel assemblies
Programmable, multi-segment heating profiles tailored to your alloy system
Full data logging and batch reporting for AS9100 and NADCAP compliance support
Our engineers work directly with customers to develop and validate brazing recipes for their specific panel configurations, so you are not starting from zero.
Ready to Bring Honeycomb Panel Brazing In-House?
If you are currently outsourcing your honeycomb panel brazing or struggling with consistency on an older furnace, Normantherm can help you take control of the process. Better quality, faster throughput, and full traceability start with the right furnace.
You may also like
Industry News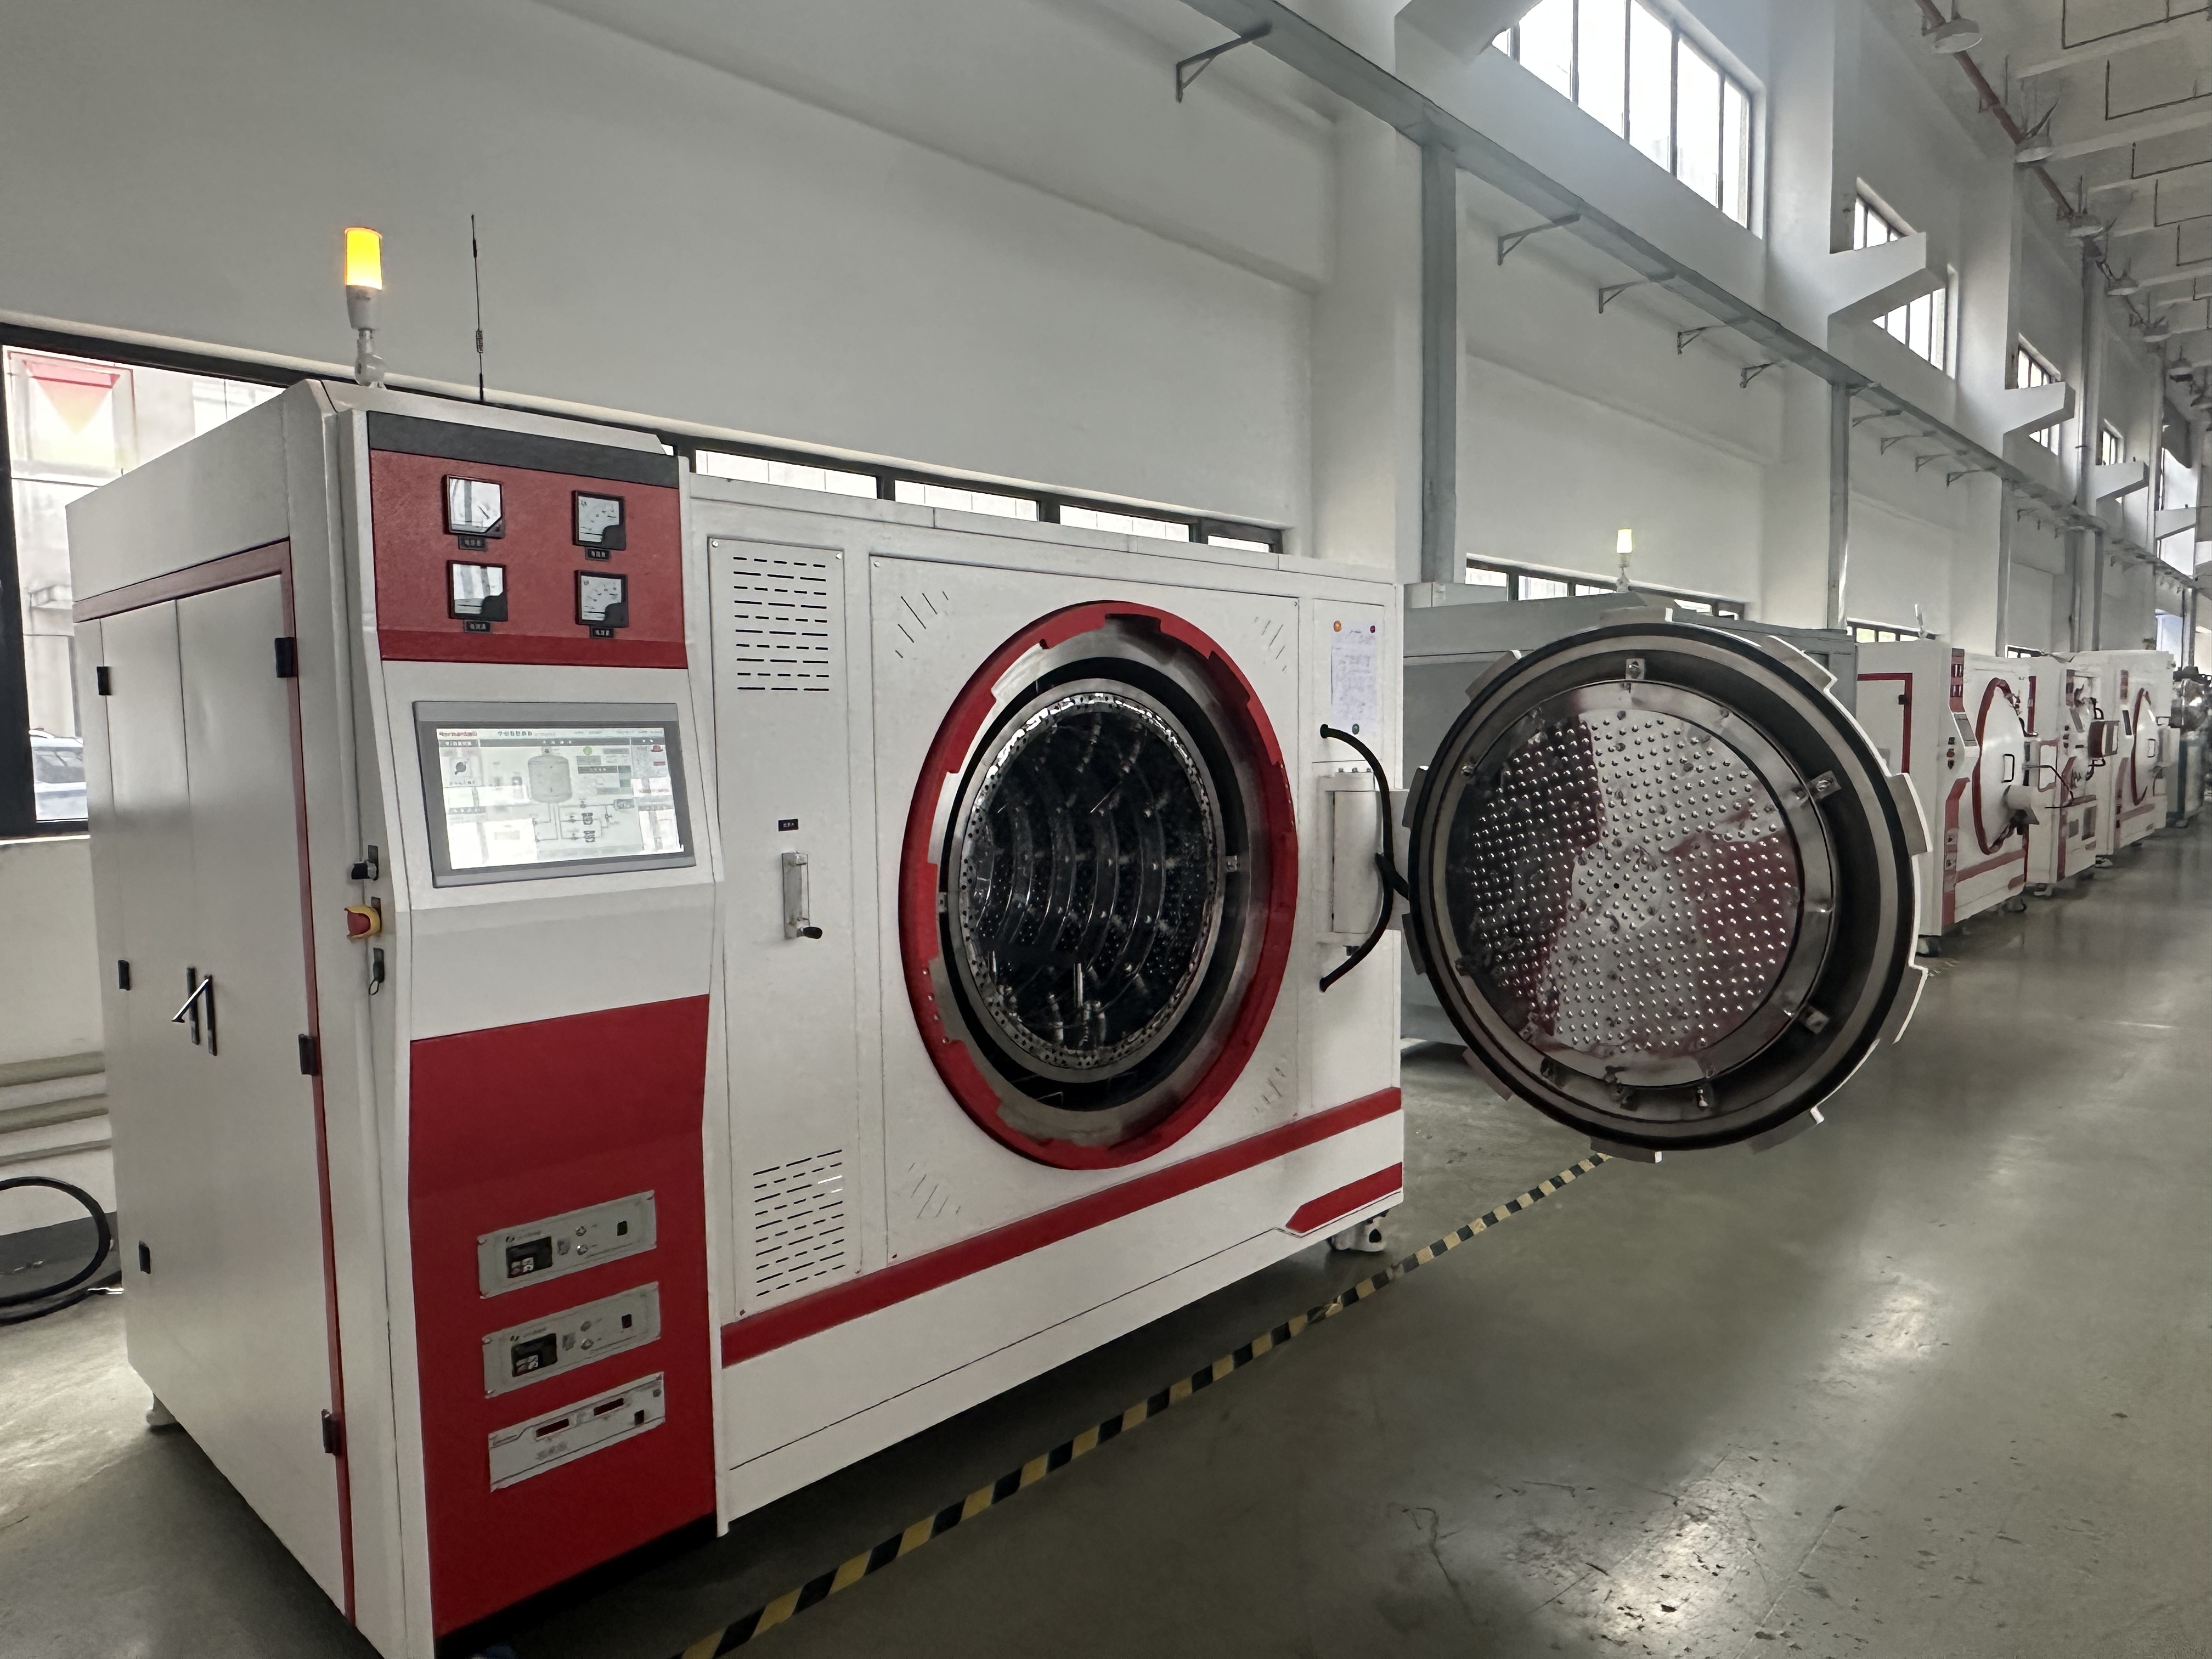 Industry News
 Industry News